Introduction: Precision Turned Components in Modern Automotive Manufacturing
The contemporary automotive sector increasingly relies on specialized manufacturer of screw-machined components for the automotive industry to deliver precision-engineered parts that standard fastener suppliers cannot accommodate. Industry data reveals that vehicle complexity has increased 400% over the past two decades, with modern automobiles containing 15,000-30,000 individual components—many requiring custom-machined geometries, tight tolerances, and exotic materials. Demand for automotive screw-machined parts is driven by powertrain electrification, advanced driver assistance systems (ADAS), and lightweighting, all of which require specialized turning capability.
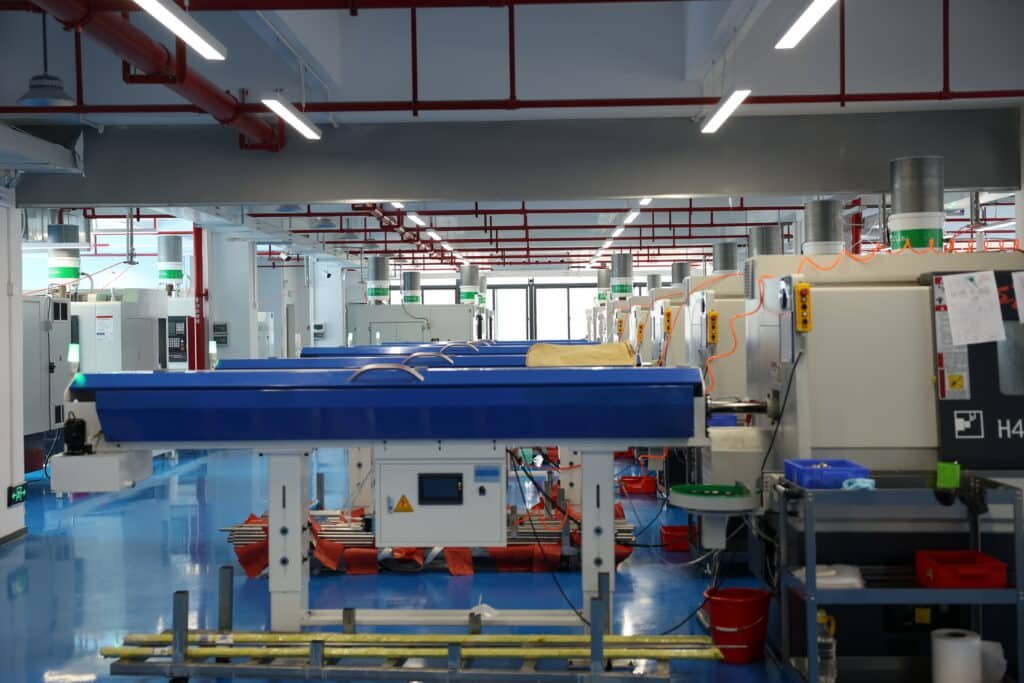
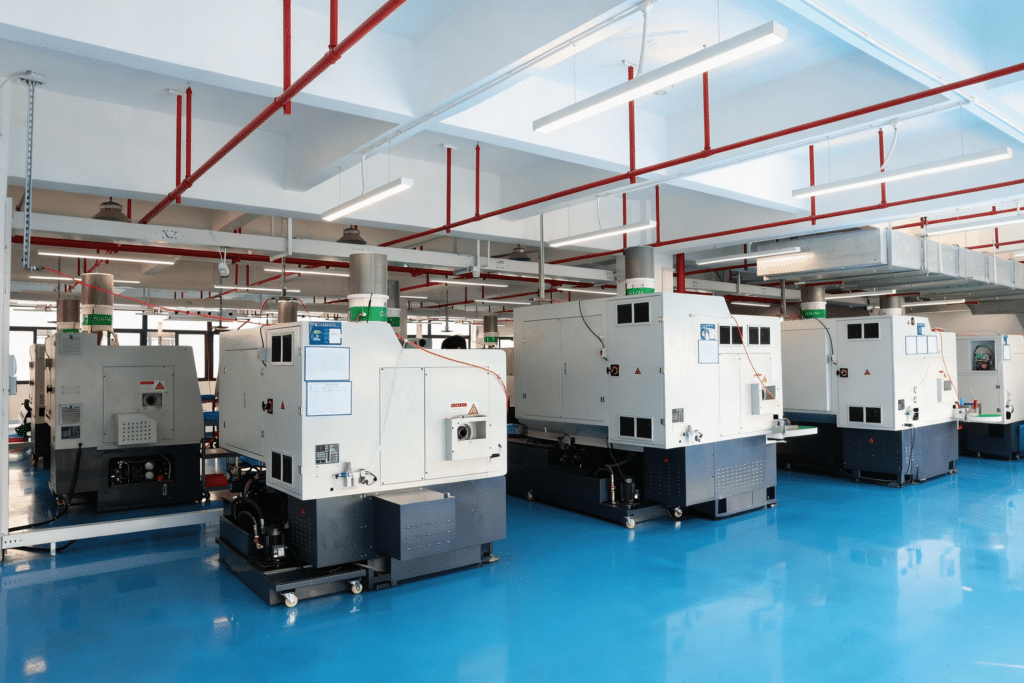
KEYFIX, established in 2005 as a precision component manufacturer, serves international automotive clients with IATF 16949:2016 certified screw-machining operations in its own 8,000 m² plant in Guangdong. Our integrated capabilities—CNC lathes and mill-turn centers holding ±0.005 mm on critical features, two YCM NFX 380A 5-axis machining centers for complex geometries, material expertise spanning carbon steel through titanium, and dimensional verification by 2D video measuring and Shining3D 3D scanning—position us as a strategic partner for automotive OEMs and tier suppliers requiring turned components beyond commodity fastener specifications.
This technical examination analyzes screw-machining technologies, automotive application requirements, material selection frameworks, and quality management systems essential for procurement engineers and product designers specifying custom-turned components in contemporary vehicle development programs.
Screw-Machining Technology Architecture
Manufacturer of screw-machined components for the automotive industry operations integrate multiple turning technologies—each optimized for specific part geometries, production volumes, and precision requirements characteristic of automotive applications.
Screw-Machining Technology Comparison Matrix
| Manufacturing Technology | Equipment Configuration | Diameter Capability | Length Capacity | Production Velocity | Precision Achievement | Optimal Volume Range |
|---|---|---|---|---|---|---|
| Swiss-Type CNC Turning | Sliding headstock, guide bushing support | Ø2mm – Ø32mm (0.079″ – 1.26″) | Up to 300mm (12″) | 8-35 parts/minute | ±0.003mm (±0.00012″) | 500 – 100,000+ units |
| Fixed-Headstock CNC Lathe | Conventional turret configuration | Ø10mm – Ø250mm (0.39″ – 9.84″) | Up to 500mm (20″) | 3-12 parts/minute | ±0.005mm (±0.0002″) | 100 – 50,000 units |
| Multi-Spindle Automatic | 6-8 spindle rotary transfer | Ø3mm – Ø65mm (0.12″ – 2.56″) | Up to 200mm (8″) | 15-60 parts/minute | ±0.010mm (±0.0004″) | 50,000 – 1,000,000+ units |
| 5-Axis Mill-Turn Center | Integrated milling capability | Ø10mm – Ø400mm (0.39″ – 15.75″) | Up to 800mm (31.5″) | 2-8 parts/minute | ±0.005mm (±0.0002″) | Prototypes – 10,000 units |
| CNC Turret Lathe | Heavy-duty construction | Ø50mm – Ø600mm (1.97″ – 23.62″) | Up to 1,500mm (59″) | 1-5 parts/minute | ±0.010mm (±0.0004″) | 50 – 5,000 units (large components) |
Swiss-Type CNC Technology represents the cornerstone capability for precision automotive screw-machined components—unique sliding headstock design positions workpiece immediately adjacent to cutting tool (within guide bushing), minimizing deflection from cutting forces critical when machining small-diameter, high-length-to-diameter-ratio parts. Typical automotive turned components include fuel injector bodies (Ø6mm × 45mm length requiring ±0.005mm concentricity), sensor housings (complex multi-diameter profiles with cross-drilling), precision shafts (surface finish Ra 0.4μm specifications), and hydraulic valve components (tight tolerance bores with chamfers).
5-Axis Mill-Turn Integration addresses automotive components requiring both turning and complex milling operations—turbocharger actuator components combining cylindrical turning with precision slot milling, transmission synchronizer parts featuring turned profiles plus indexed hole patterns, electric motor shafts requiring turning plus keyway machining. KEYFIX’s two YCM NFX 380A 5-axis machining centers eliminate multiple setups (single-operation complete machining), reduce tolerance stackup errors (all features machined in one workholding), and accelerate prototype-to-production transitions. Typical applications include EV battery cooling system components, ADAS sensor mounting brackets, and brake system hydraulic fittings demanding geometric complexity exceeding pure turning capabilities.
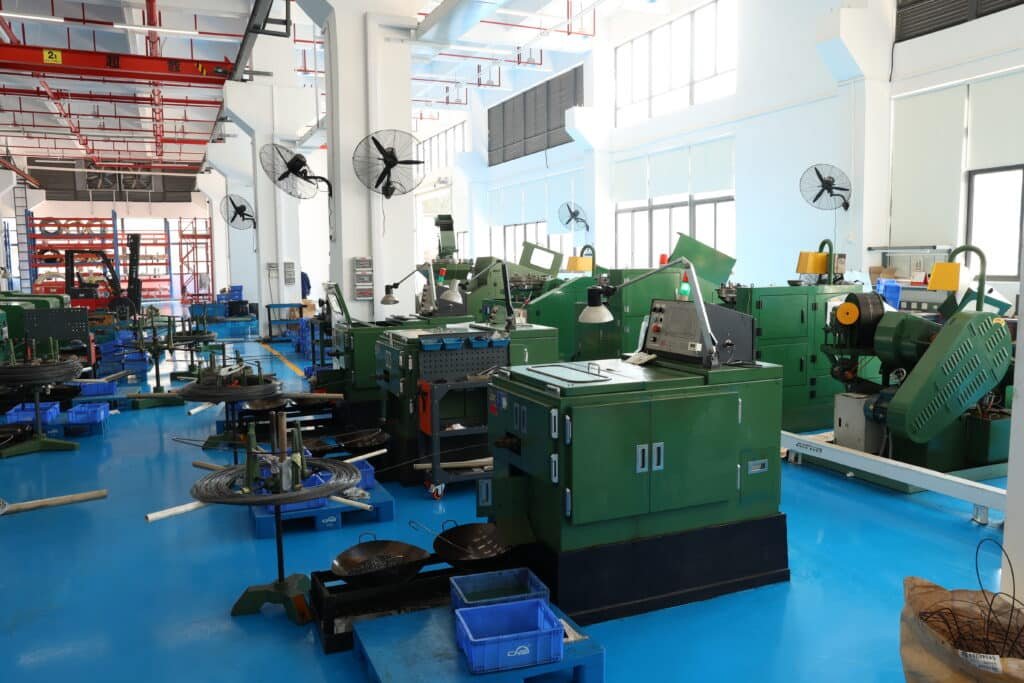
Multi-Spindle Automatic Screw Machines deliver maximum production efficiency for high-volume automotive components—6-8 spindles simultaneously machine identical parts from bar stock, with rotary transfer indexing workpieces through progressive cutting stations. While offering lower precision versus Swiss-type equipment (±0.010mm typical), multi-spindle technology excels in cost-per-piece economics above 50,000 annual volume.
Automotive Application Engineering Requirements
Different vehicle systems impose distinct technical demands on screw-machined components—understanding these requirements enables manufacturer of screw-machined components for the automotive industry to optimize designs for manufacturability while ensuring functional performance.
Automotive System Requirements Analysis
| Vehicle System | Representative Screw-Machined Components | Critical Technical Requirements | Material Specifications | Typical Tolerances |
|---|---|---|---|---|
| Fuel Systems | Injector bodies, rail connectors, pressure regulators | High-pressure sealing (2,000+ bar), corrosion resistance | Stainless 316L, precipitation-hardening 17-4 PH | ±0.005mm on sealing surfaces |
| Transmission | Synchronizer components, valve bodies, shaft couplings | Wear resistance, precise concentricity, thermal stability | Case-hardened 8620, nitrided 4140 alloy steel | ±0.003mm concentricity, Ra 0.4μm finish |
| Brake Systems | ABS valve components, master cylinder pistons, calipers | Hydraulic compatibility, corrosion protection, fatigue strength | Stainless 304/316, aluminum 6061-T6 | ±0.008mm diameter, ±0.5μm surface finish |
| Electric Powertrain | Motor shaft components, inverter heat sink mounts, battery cooling fittings | Lightweight, electrical conductivity/isolation, thermal management | Aluminum 7075-T6, brass C360, titanium Grade 5 | ±0.005mm on critical fits |
| ADAS Sensors | Camera housings, radar mounts, lidar brackets | Precision positioning, vibration damping, EMI shielding | Aluminum anodized, brass, stainless 304 | ±0.010mm positioning accuracy |
| Steering Systems | Rack components, column bushings, electric assist motor parts | Low friction, wear resistance, precise geometry | Bronze alloys, case-hardened steel, engineered polymers | ±0.005mm on bearing surfaces |
Fuel System Component Engineering demands exceptional precision—common rail diesel injectors operate at 2,000-2,500 bar injection pressure requiring seal surface flatness <0.002mm and concentricity ±0.003mm preventing high-pressure leakage. For fuel injector bodies in 17-4 PH stainless steel, the typical route is CNC turning of the primary diameter to ±0.005 mm, reaming internal passages, and cross-drilling inlet ports with carbide tooling to prevent burrs. Post-machining passivation per ASTM A967 enhances corrosion resistance against diesel fuel sulfur content and water contamination.
Transmission Component Complexity requires multi-operation screw-machining—synchronizer sleeves combining external splines (machined via hobbing after turning), precision bores (ground to ±0.002mm), and face perpendicularity (±0.005mm relative to bore centerline). These components follow staged manufacturing: CNC rough-turning, secondary boring of precision internal diameters, then grinding, hobbing or honing to specification for final diameter, spline profile and bearing-surface finish. Material selection typically specifies 8620 case-hardening steel, carburized to 58-62 HRC surface hardness while maintaining 30-35 HRC ductile core.
Electric Vehicle Thermal Management introduces new screw-machined component categories—battery cooling system manifolds distributing coolant across cell modules, inverter cold plates featuring internal cooling passages, motor rotor shafts requiring precision balancing. Aluminum dominates due to excellent thermal conductivity (205 W/m·K for 6061 alloy versus 50 W/m·K for steel) and 65% density reduction supporting vehicle lightweighting. KEYFIX machines EV thermal components from 6061-T6 and 7075-T6 aluminum through specialized cutting parameters: slower surface speeds (150-250 SFM) preventing work-hardening, aggressive feed rates promoting chip evacuation, high-pressure coolant (1,000+ psi) managing heat concentration in low-thermal-conductivity material, and sharp carbide tooling geometries minimizing cutting forces that deflect soft aluminum workpieces.
Material Science and Alloy Selection
Manufacturer of screw-machined components for the automotive industry must maintain comprehensive material expertise—automotive applications span complete material property spectrum from economical carbon steels to exotic high-temperature alloys.
Comprehensive Material Selection Guide
| Material Category | Representative Alloys | Machinability Rating | Strength Characteristics | Automotive Applications | Cost Index |
|---|---|---|---|---|---|
| Free-Machining Steel | 12L14, 1215, 1144 | Excellent (100% baseline) | 60-90 ksi tensile, good fatigue | Sensor brackets, mounting pins, general hardware | 1.0× |
| Carbon Steel | 1018, 1045, 1141 | Good (70-80%) | 70-120 ksi, heat-treatable | Structural components, shafts, couplings | 1.1× |
| Alloy Steel | 4140, 4340, 8620 case-hardening | Fair to good (60-75%) | 150-220 ksi heat-treated | Transmission parts, high-stress components | 1.5× |
| Stainless Austenitic | 303, 304, 316, 316L | Good (60-70%) with proper tooling | 75-95 ksi, excellent corrosion resistance | Fuel systems, brake components, exterior | 3.2× |
| Stainless Precipitation-Hardening | 17-4 PH, 15-5 PH | Fair (50-60%) | 145-190 ksi after aging | High-strength corrosion-critical parts | 4.5× |
| Aluminum Alloys | 6061-T6, 7075-T6, 2024-T4 | Excellent (90-95%) | 35-83 ksi, lightweight | EV components, heat sinks, brackets | 2.0× |
| Brass/Bronze | C360 brass, C932 bearing bronze | Excellent (100%+) | 50-90 ksi, low friction | Bushings, electrical contacts, wear surfaces | 3.8× |
| Titanium | Grade 2 CP, Ti-6Al-4V (Grade 5) | Poor (20-30%) challenging | 50-145 ksi, 43% of steel density | Racing, premium EVs, weight-critical | 15.0× |
Free-Machining Steel Optimization for high-volume automotive production—12L14 leaded steel (0.15-0.35% lead content) provides superior chip breaking and excellent surface finish (Ra 0.8μm achievable) enabling aggressive cutting parameters and extended tool life. However, environmental regulations increasingly restrict lead usage (RoHS compliance, California Proposition 65), driving adoption of lead-free alternatives: 1215 rephosphorized steel (0.04-0.09% phosphorus enhancing machinability), 1144 resulfurized steel (0.24-0.33% sulfur improving chip formation). KEYFIX stocks multiple free-machining grades enabling material selection optimized for each application: 12L14 for cost-sensitive components in non-regulated markets, 1215 for RoHS-compliant applications, 1144 for applications requiring moderate strength with excellent machinability.
Stainless Steel Machining Expertise differentiates advanced screw-machine shops from basic turning operations—austenitic stainless (304, 316 families) work-hardens rapidly during cutting, requires sharp tooling geometries (positive rake angles), generous coolant application preventing heat buildup, and reduced cutting speeds (60-120 SFM versus 200-300 SFM for carbon steel). KEYFIX machines stainless automotive components through specialized strategies: ceramic or coated carbide insert tooling resisting heat and chemical wear, high-pressure coolant delivery (1,500 psi through-spindle systems) directly cooling cutting zone, aggressive feed rates (0.012-0.020 IPR) promoting chip evacuation before work-hardening occurs, and rigid workholding minimizing vibration-induced tool deflection. Material certificates per ASTM A479 accompany all stainless screw-machined components validating chemistry and mechanical properties.
Titanium Screw-Machining Challenges require specialized expertise—low thermal conductivity (17 W/m·K versus 50 W/m·K for steel) concentrates cutting heat at tool-workpiece interface degrading both tool and material, chemical reactivity with cutting tool materials at elevated temperature, work-hardening tendency during deformation. KEYFIX approaches titanium automotive components (racing suspension components, premium EV lightweight parts) through dedicated processes: very low cutting speeds (40-80 SFM), carbide tooling with TiAlN or diamond-like coatings, flood coolant with EP (extreme pressure) additives, and frequent tool indexing preventing excessive wear. While titanium machining costs 8-12× carbon steel per hour, resulting 43% weight savings justify economics in performance and luxury vehicle applications.
Quality Management and Validation Systems
Automotive screw-machined component applications demand PPM-level quality—a manufacturer of screw-machined components for the automotive industry must implement comprehensive validation protocols ensuring dimensional accuracy, material integrity, and functional performance.
Integrated Quality Assurance Framework
| Quality System Element | Implementation Technology | Inspection Standards | Validation Frequency | Documentation Requirements |
|---|---|---|---|---|
| Material Verification | Spectroscopic analysis (OES) | ASTM E415 elemental composition | 100% incoming lot verification | Mill certificates + confirmatory testing |
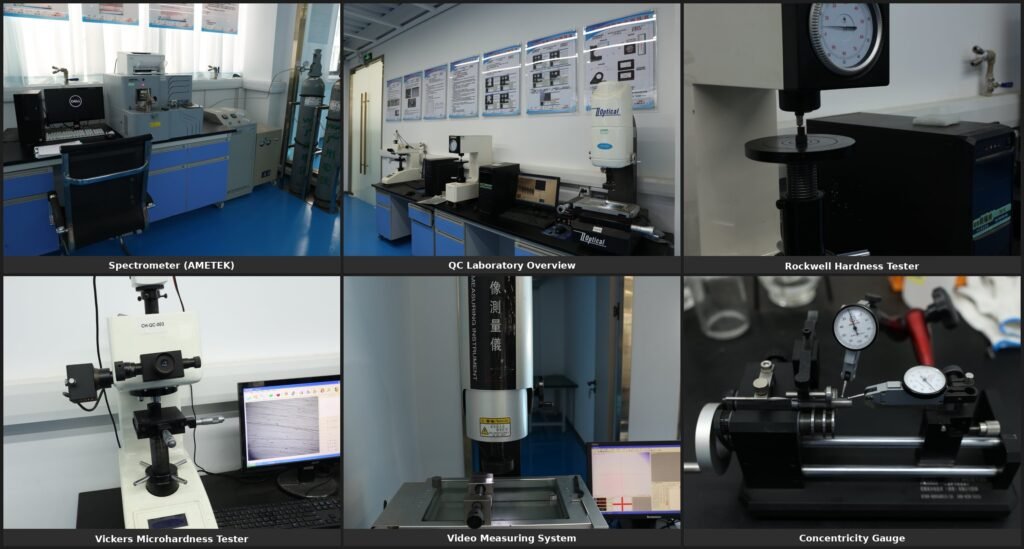
| Dimensional Conformance | 2D video measuring system, Shining3D 3D scanner | ISO 1101 GD&T, ASME Y14.5 | First article + statistical sampling (5%) | Actual measurements vs. nominal specifications |
| Surface Finish Validation | Surface roughness measurement (on request) | ISO 4287 Ra, Rz, RSm parameters | First article + periodic sampling | Surface texture trace records |
| Concentricity/Runout | Indicator gauging, 2D video measuring | ISO 1101 geometric tolerancing | Critical features 100% or statistical | TIR (Total Indicator Reading) data |
| Thread Geometry | Thread micrometers, optical comparators | ASME B1.1, ISO 965-1 standards | Setup validation + shift checks | Pitch diameter, major/minor diameter records |
| Hardness Testing | Rockwell, Vickers, microhardness | ASTM E18, E384 procedures | Heat-treated parts per batch (3+ samples) | Hardness traverse data, case depth verification |
| Statistical Process Control | Real-time SPC software integration | Cpk ≥1.67 process capability | Continuous monitoring during production | Control charts, capability indices, corrective actions |
| First Article Inspection | Complete dimensional + functional | AS9102, PPAP Level 3/4/5 | New parts, engineering changes, annual | FAI reports, balloon drawings, characteristic matrix |
IATF 16949:2016 Compliance validates KEYFIX’s organizational maturity meeting automotive industry quality management requirements—advanced product quality planning (APQP) methodology structures screw-machined component development from concept validation through production launch, production part approval process (PPAP) provides comprehensive first-article validation before production authorization, failure mode and effects analysis (FMEA) systematically identifies machining process risks implementing preventive controls, measurement system analysis (MSA) ensures inspection equipment contributes minimal variation to total measurement uncertainty. NQA conducts annual surveillance audits validating sustained compliance and continuous improvement culture supporting multi-year automotive supply agreements.
Coordinate Measuring Machine (CMM) Inspection is the industry reference method for complex geometries. Typical automotive inspection protocols measure: diameter features at multiple locations (minimum 3 points per diameter establishing cylindricity), perpendicularity of machined faces relative to datum features, positional tolerance of cross-drilled holes, concentricity between multiple turned diameters, and surface finish across critical functional surfaces. KEYFIX verifies these features with a 2D video measuring system (0.001 mm optical measurement resolution), Shining3D 3D scanning for color-mapped deviation analysis against CAD models, and 145 Mitutoyo precision gauges—identifying systematic machining errors before significant non-conforming production accumulates.
Statistical Process Control (SPC) Implementation enables proactive quality management—KEYFIX monitors critical dimensions in real-time during CNC production: primary diameter measurements plotted on X-bar and R charts with automated alerts when measurements trend toward specification limits, tool wear compensation tracking offsetting predictable dimensional drift, and process capability studies (Cpk calculations) validating manufacturing stability. Target Cpk ≥1.67 ensures processes remain centered within specification windows with minimal variation—statistically confirming <63 defects per million opportunities (6-sigma quality level). SPC data integration with machine tool controllers enables automated tool offset adjustments maintaining dimensions within ±0.002mm target ranges throughout extended production runs.
Supplier Partnership Framework: KEYFIX Competitive Advantages
Selecting a manufacturer of screw-machined components for the automotive industry requires systematic evaluation across technical capabilities, automotive industry experience, and quality system maturity—transactional purchasing risks supply disruptions and quality failures.
Comprehensive Supplier Evaluation Matrix
| Assessment Dimension | Commodity Screw-Machine Shops | KEYFIX Specialized Automotive Capability | Strategic Customer Value |
|---|---|---|---|
| Automotive Quality Certification | ISO 9001 general quality baseline | IATF 16949:2016 + ISO 14001:2015 environmental | OEM-qualified supplier status, comprehensive PPAP |
| Precision Capability | ±0.010mm typical tolerance | ±0.005 mm Swiss-type CNC, ±0.01 mm cold forging | Eliminates secondary grinding operations |
| Equipment Sophistication | Manual or basic CNC lathes | 32 CNC machines incl. Swiss-type lathes, mill-turn and 2 × YCM 5-axis | Complex geometry capability, single-setup complete |
| Material Expertise | Steel and basic stainless only | Carbon/alloy steel, stainless variants, aluminum, brass, titanium | Comprehensive solution source, optimal material selection |
| Production Flexibility | High-volume only, 25,000+ MOQ | 500-5,000 MOQ for custom development | Prototype-to-production continuity without supplier changes |
| Engineering Collaboration | Order fulfillment focus only | DFM analysis, tolerance rationalization, cost optimization | Value engineering partnership, 15-25% typical cost reduction |
| Lead Time Performance | 8-12 weeks production cycles | Typically 7–14 business days samples, 4–6 weeks production | Compressed development schedules, faster time-to-market |
| Global Automotive Experience | Regional supplier limitations | 20+ years of automotive export programs | International standards understanding, export compliance |
This specialized equipment concentration enables: economies of scale reducing setup and programming costs, accumulated operator expertise optimizing cycle times and tool life, standardized fixturing libraries accommodating rapid changeovers, and comprehensive spare parts inventory minimizing unplanned downtime. Competitive screw-machine shops operating 2-3 Swiss-type machines among mixed conventional equipment lack volume concentration justifying this infrastructure investment and process optimization depth.
Engineering Collaboration drives component improvement—KEYFIX engineers review screw-machined component designs (integrated features, simplified geometries), machining process choices (toolpath optimization, work-holding), and inspection methods (in-process measurement, statistical sampling) through a free DFM review on every new part number. A typical example: combining a turned body, cross-drilled cable passage, and machined mounting surface into a single-setup part eliminates assembly operations while improving positional accuracy versus multi-piece alternatives.
Complete value chain coordination—KEYFIX handles material procurement, precision machining (CNC turning, mill-turn and 5-axis), secondary operations (thread rolling, grinding, heat treatment), surface finishing (plating, coating, passivation), quality validation (dimensional, material, functional testing), and logistics (packaging, export documentation, delivery). This turnkey approach versus managing multiple suppliers reduces customer administrative burden while providing single-point accountability for quality, delivery, and total cost performance.
Conclusion: Strategic Partnership for Automotive Screw-Machining Excellence
Contemporary automotive development demands manufacturer of screw-machined components for the automotive industry combining precision manufacturing capability, comprehensive material expertise, automotive quality systems, and collaborative engineering support. Vehicle complexity growth, powertrain electrification, advanced safety systems integration, and lightweighting imperatives create increasing demand for custom-turned components exceeding commodity fastener specifications—yet procurement decisions frequently emphasize unit price over strategic supplier capabilities risking quality issues and development delays.
KEYFIX’s 20+ years of precision component manufacturing integrate CNC turning (±0.005 mm), 5-axis machining (2 × YCM NFX 380A), IATF 16949:2016 certified quality management, a broad automotive material portfolio (carbon and alloy steel, stainless, aluminum, brass, titanium), and AQL 0.4 outgoing inspection with a target below 25 PPM. Our 32 CNC machines, 2D video measuring and 3D scanning, and complete value chain integration position us as a strategic manufacturing partner versus a transactional supplier.
Engage KEYFIX’s automotive engineering team to evaluate screw-machined component requirements—we provide complimentary design for manufacturability analysis identifying cost optimization opportunities, rapid prototype development delivering functional samples typically within 7–14 business days enabling design validation, comprehensive testing services (dimensional, material, functional performance), and complete PPAP documentation supporting OEM qualification processes with dimensional validation, process capability studies, and material property verification.
Request capability assessment demonstrating KEYFIX precision screw-machining expertise—sample parts showing ±0.005 mm tolerance achievement and surface finish quality, facility documentation including equipment lists and quality system certifications, or virtual facility tours examining CNC turning operations, 5-axis machining centers, inspection equipment, and the quality management infrastructure behind our automotive production.